Folding Carton Closures: Tuck End, Lock Bottom or Auto Bottom?
Quick answer
Choose a folding carton closure around the filled product, the packing method and the way the customer opens it. Tuck ends, manually locked bottoms and pre-glued auto bottoms solve different assembly problems. None has a universal load capacity. Compare physical samples using the same product and board specification, then approve the closure, insert and artwork together before production.
Packaging design reference. Final fit, materials and finish are confirmed on an approved sample.
At a glance
Compare folding carton closures by product weight, packing method and opening. Use a sample checklist to choose a workable structure before artwork approval.
A bottle loaded from the top places different demands on the base from a light accessory loaded through either end. Record the filled weight, base shape, sharp edges, cap position and intended display orientation. Include any leaflet or insert: it can obstruct the closing flap even when the product itself fits.
State whether operators will assemble the carton by hand or use a packing line. For a line, share the equipment requirements and loading direction with the converter before the dieline is approved. A closure that works on a desk is not automatically compatible with production equipment.
02
Compare closure behavior
Closure selection before sampling
Closure
When to investigate it
What must be checked
Tuck end
An accessible opening for relatively simple loading and removal
Flap retention, friction, product interference and opening direction
Manual lock bottom
A base assembled by interlocking flaps
Assembly sequence, complete engagement and stability under the actual load
Pre-glued auto bottom
A carton whose base forms as the sleeve is opened
Glue joints, full opening, base seating and compatibility with the filling process
These are selection starting points, not load ratings. Ask the supplier to identify the exact closure on the drawing because informal names such as “crash lock” can be used inconsistently. Keep the dieline revision beside the material specification.
03
Specify board and creases together
Board thickness, stiffness, coating and crease design all affect how a carton folds. Increasing grammage alone may make a flap harder to insert or change the finished fit. Request the board grade and thickness alongside GSM; compare a production-representative sample rather than choosing from a weight number alone.
Pro Carton describes carton manufacture as a sequence including printing, cutting, creasing and folding/gluing. The practical implication for the buyer is that the printed sheet and the assembled box need separate checks. Inspect fold edges for visible damage and verify that decoration near a crease still meets the agreed appearance reference. See the board specification guide for the difference between material descriptions.
04
Check the product and insert as one assembly
A carton may close when empty and bow when loaded. If the insert lifts the bottle, the cap can press on the lid; if the base is narrow, the load may concentrate at an unsupported point. Review the complete loaded carton upright and in the orientations expected during packing. Do not use the top flap to force an oversized product into place.
For a pump bottle, check actuator and cap clearance separately. Product support should come from a deliberately designed base or insert, not accidental pressure on a pump. The carton also needs external transport protection when the distribution route requires it.
05
Run a repeatable sample comparison
Assemble several samples using the proposed packing instructions; record any ambiguous fold or missed lock.
Load the actual filled product, insert and leaflet, then close without distorting the panels.
Inspect base engagement and glue areas, and agree a load-handling evaluation with the supplier.
Open and remove the product as a customer would; check tearing, snagging and access.
Review a printed sample for cracking, scuffing and artwork hidden by flaps.
If comparing assembly effort, use the same packing task and document the conditions. Do not assume an auto bottom saves a particular number of seconds without observing the actual operation. A faster assembly can still be unsuitable if product positioning becomes unreliable.
06
Freeze the closure before final artwork
Changing a bottom or flap after artwork approval can move folds, glue areas and panel boundaries. Confirm the structure first, issue artwork on the approved dieline, and retain a signed or otherwise traceable assembled reference. Record the loading direction in the pack-out instructions so a later team does not reverse it.
Pro Carton: carton production explains the manufacturing stages. Closure suitability and load performance remain project-specific and require sample evaluation; no test result is claimed here.
From guide to product
Compare packaging for your brief
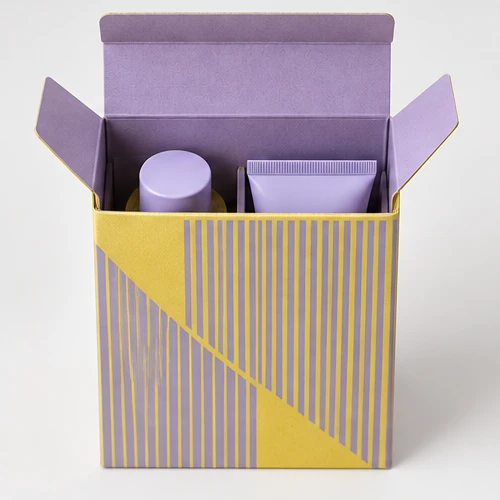
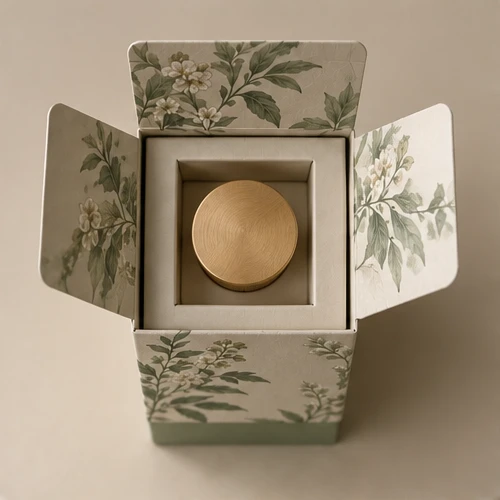
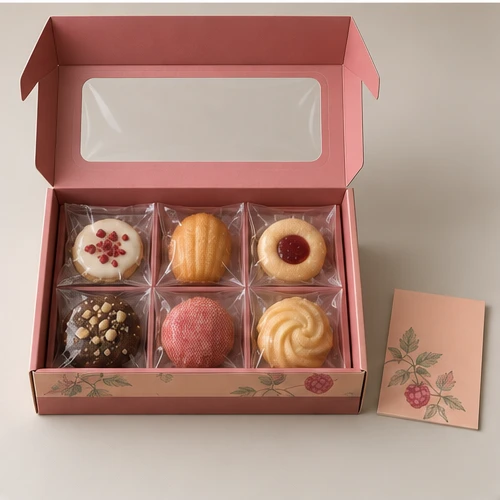
Explore the opening, material and insert details for each design. These are options to review, not proof of a tested fit for your product.
 Bank Transfer
 PayPal