Custom Packaging Inspection Checklist: Samples, Defects and AQL
Quick answer
Before inspecting custom packaging, agree what will be checked, which production lot it belongs to and what evidence permits shipment. Use an approved sample together with a written specification, a defect catalogue and an agreed sampling plan. Record measurements and observed defects separately from the release decision. A good-looking sample alone cannot establish that the production lot meets your requirements.
Packaging design reference. Final fit, materials and finish are confirmed on an approved sample.
At a glance
Plan a custom packaging inspection: approved samples, defect classes, AQL inputs, functional checks and shipment release records for boxes and paper bags.
Separate sample approval from production inspection
An approved sample answers a design question: is this the structure, fit and appearance the buyer wants? Production inspection answers a different question: does the identified lot meet the agreed acceptance criteria?
Keep a dated, labelled reference sample with its drawing revision, artwork version and approval notes. State any exceptions. If a hand-made sample uses a different board or finishing process from production, record the difference instead of treating every feature as a production standard. See the custom packaging sampling process for the earlier approval stage.
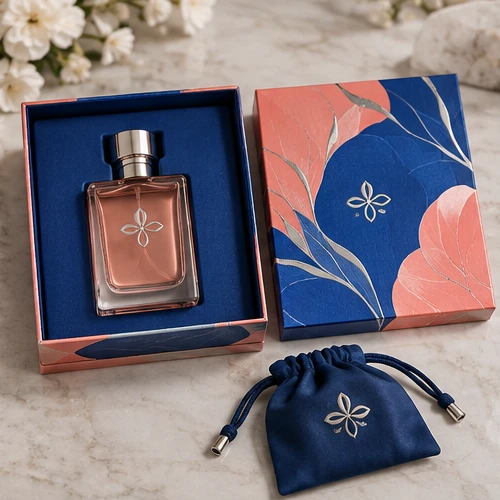
For example, a perfume box can match the approved foil colour but still grip the bottle too tightly. Approving the decoration should not automatically approve the insert fit. Check these characteristics independently.
02
Freeze the specification before choosing the inspection plan
A useful inspection brief identifies the purchase order, SKU, quantity, lot boundaries, drawing and artwork revisions, approved reference and person authorised to release shipment. Separate products or production runs where their risks or specifications differ; do not quietly combine them into a convenient inspection total.
List the measurement method beside each requirement. “Correct size” is incomplete: specify internal or external dimensions, measurement locations, assembled condition and agreed tolerances. “Correct colour” needs the physical reference and viewing conditions; an uncontrolled phone photograph should not be the sole acceptance reference.
Rigid boxes: identify lid fit, insert location, wrapped edges and any magnetic closure.
Folding cartons: identify crease behaviour, glued seams, closure engagement and compatibility with the packing method.
Paper bags: identify handle attachment, base construction and the intended loaded configuration.
Agree product-specific limits with the responsible technical team. This guide does not prescribe a universal dimensional tolerance or load rating. Record later changes using packaging specification change control.
03
Create a defect catalogue that inspectors can actually use
Use labelled photographs or retained samples to define the boundary between acceptable and unacceptable workmanship. Include the inspection distance, lighting, location and severity where relevant. A mark on a hidden base and the same mark across a visible logo may need different decisions.
The following is a buyer planning framework, not a classification table from an inspection standard. Assign each actual defect before inspection, based on its consequence and the product's requirements.
Illustrative defect classification for a packaging brief
Class
Decision to document
Possible packaging example
Critical
A safety or applicable compliance concern requiring a defined hold and escalation rule.
A sharp foreign object in the pack. Determine the response with the responsible safety team.
Major
A defect that defeats the agreed use or makes the pack unacceptable for sale.
An insert that prevents the approved bottle from fitting, or an incorrect SKU printed on the carton.
Minor
A limited workmanship departure that does not defeat the agreed function.
A small cosmetic mark outside the principal display area, if the approved catalogue classifies it that way.
Do not change a defect from major to minor after counting it simply to obtain a pass. Safety concerns need an explicit response even if other appearance results meet their sampling criteria.
04
Specify AQL inputs instead of writing only “AQL inspection”
Acceptance sampling uses observations from a random sample to make a decision about a lot. It does not inspect every unit or guarantee that every unexamined item conforms. NIST distinguishes the lot acceptance decision from estimating the quality of the lot. Source: NIST, What is Acceptance Sampling?
AQL means acceptance quality limit. ISO currently lists ISO 2859-1:2026 for AQL-indexed inspection by attributes. ASQ describes ANSI/ASQ Z1.4-2003 (R2018) as a system for continuing lots with switching rules, supporting percent nonconforming or nonconformities per 100 units. Identify the standard and edition agreed for the order; do not mix tables or rules from different systems.
Ask the qualified inspector or quality lead to document:
The defined lot size and inspection unit: one box, one component or one complete set.
The standard, edition, inspection level and applicable normal, tightened or reduced status.
The agreed AQL for each applicable defect class, plus any separate critical-defect hold rule.
The selected sampling plan, sample size and acceptance/rejection numbers taken from that plan.
The random selection method across the lot and the separate scope of functional or destructive tests.
“AQL 2.5” alone is not a complete inspection instruction. It is not a promise that exactly 2.5% of a delivered shipment will be defective. This article does not reproduce sampling tables or choose thresholds for an order; those decisions require the applicable standard and an agreed plan.
05
Count defective units and individual defects consistently
One unit can contain more than one defect. Agree the counting basis before inspecting and keep separate results for each applicable severity class. Otherwise two inspectors can record the same observations differently.
Illustrative arithmetic only: suppose a teaching example contains 100 inspected boxes. Four boxes are nonconforming; one of those four has two recorded defects and the other three have one each. That produces 4 nonconforming units and 5 defects.
Percent nonconforming: 4 ÷ 100 × 100 = 4%.
Nonconformities per 100 units: 5 ÷ 100 × 100 = 5.
These invented counts explain two recording methods. They are not MTT inspection results, a recommended sample size or an AQL acceptance example. A pass or fail cannot be inferred from these figures without the chosen plan and defect classification.
06
Check function as well as appearance
Build the inspection around the product that will actually be packed. If the actual product is unavailable, record what substitute was used and which conclusions remain unverified. A display mock-up should not silently stand in for a filled glass bottle when checking retention or handling.
Practical checkpoints to adapt to the approved packaging specification
Checkpoint
What to observe
Evidence to keep
Product fit
Insertion, removal, contact points and the agreed retention method.
Product identity, dimensions, photos and measured results.
Assembly and closure
Carton erection, lid seating, drawer travel or handle attachment, as applicable.
Test method, repetitions if specified, sample IDs and failures.
Print and finish
Artwork revision, text, logo position, foil coverage and agreed visual limits.
Approved reference, defect location and comparable images.
Outer packing
SKU separation, count, orientation, protection and shipping marks.
Carton IDs, packing list checks and packed configuration.
For fragile products, assess transport performance separately using the agreed packed system and test method. A visual inspection of empty gift boxes cannot establish transit protection for the filled pack. The shipping carton specification guide explains the outer-pack decisions; the insert guide covers fit and support.
07
Make the report traceable to the shipment decision
A report should let the buyer connect every finding to a requirement and an inspected unit. Retain the lot and carton identifiers, selection method, sample count, inspection date, inspector, reference revisions, instruments where relevant, readings, defect photographs and result by class. Record tests not performed as not performed.
Use a short finding record: requirement → sample ID → observation → classification → disposition. For a fit issue, this might describe the specified product and insert revision, the affected sample, the observed interference and the hold decision. Attach the actual measurement or image; do not replace missing evidence with a green tick.
If a lot fails, keep it on hold while the authorised parties agree sorting, rework, replacement or another documented disposition. Identify the corrected lot and agree reinspection before release. Do not obtain a pass by repeatedly taking new samples from an unchanged rejected lot. Record any concession, its scope and who accepted it.
Before dispatch, reconcile the inspection report with the exact goods being shipped. A report for a different revision or an earlier lot does not automatically cover this shipment. Start the next order with the approved specification and the recorded corrective actions, rather than only the previous invoice.
08
Sources and evidence boundaries
Prepared by MTT Packaging editorial. Official public sources checked on 8 October 2026:
The packaging checklists and defect examples are editorial planning guidance. They are not extracted standard requirements, laboratory results or customer case studies. The arithmetic example is hypothetical. Order-specific tolerances, safety requirements and sampling decisions must be agreed with the responsible technical and inspection teams.
From guide to product
Compare packaging for your brief
Explore the opening, material and insert details for each design. These are options to review, not proof of a tested fit for your product.
 Bank Transfer
 PayPal